Executive Summary
Predictive maintenance is helping pharmaceutical manufacturers move beyond fixed maintenance schedules and reactive repairs toward data-driven equipment management. By analyzing sensor readings, equipment histories, operating conditions, and performance trends, manufacturers can identify potential failures before they disrupt production.
The approach is particularly valuable in pharmaceutical environments, where equipment reliability affects product quality, batch consistency, manufacturing capacity, and regulatory compliance. Unexpected failures involving filling lines, tablet presses, HVAC systems, or critical utilities can delay production and create costly investigations.
Artificial intelligence (AI), industrial Internet of Things (IIoT) sensors, and advanced analytics are expanding predictive maintenance capabilities. However, success depends on reliable data, validated systems where required, appropriate engineering controls, and integration with existing maintenance and quality processes.
Why Is Predictive Maintenance Important in Pharmaceutical Manufacturing?
Pharmaceutical manufacturing relies on interconnected equipment operating within defined process and environmental parameters. Equipment failures can interrupt production, affect critical process conditions, delay batch release, and increase maintenance costs.
Traditional preventive maintenance reduces some risks by servicing equipment at predetermined intervals. However, time-based schedules may lead to unnecessary maintenance when equipment remains in good condition, or fail to prevent breakdowns that occur between scheduled interventions. Reactive maintenance, meanwhile, can result in unplanned downtime and urgent repairs.
Predictive maintenance uses equipment condition and performance data to estimate when intervention may be necessary. Instead of servicing every asset according to the same schedule, manufacturers can prioritize maintenance based on observed degradation, operational risk, and equipment criticality.
This approach can improve asset availability and resource allocation while supporting more consistent manufacturing operations.
How Does Predictive Maintenance Work?
Predictive maintenance combines equipment monitoring, historical records, and analytical models to identify patterns associated with developing faults.
Sensors and control systems may capture vibration, temperature, pressure, motor current, flow rates, and other operating parameters. Maintenance records, alarm histories, equipment configurations, and production conditions provide additional context.
Analytics then identify abnormal behavior, compare current readings with expected operating patterns, or estimate the likelihood of failure. Maintenance teams can investigate alerts, determine the appropriate intervention, and document the resulting work.
A typical process involves:
- Collecting relevant equipment and operating data.
- Establishing normal performance patterns and failure indicators.
- Detecting anomalies or estimating remaining useful life where sufficient evidence exists.
- Assessing the risk and urgency of maintenance.
- Scheduling interventions and reviewing outcomes to improve future predictions.
Not every alert indicates an impending failure. Models require ongoing evaluation, and predictions must be interpreted alongside engineering expertise and equipment-specific knowledge.
Which Pharmaceutical Manufacturing Assets Benefit Most?
Predictive maintenance is especially valuable for equipment whose failure could interrupt production, compromise critical conditions, or create substantial recovery costs.
HVAC and cleanroom systems
Heating, ventilation, and air-conditioning systems help maintain environmental conditions required for pharmaceutical operations. Monitoring fan performance, filter pressure differentials, airflow, and temperature can help identify deterioration before it causes significant disruption.
Because environmental controls may affect product protection and contamination control, maintenance decisions must follow established procedures and quality requirements.
Manufacturing and packaging equipment
Tablet presses, granulators, mixers, coating systems, filling machines, and packaging lines contain motors, bearings, pumps, drives, and other components that can degrade over time. Vibration and temperature trends may reveal mechanical wear, while operating data can highlight abnormal cycle times or recurring stoppages.
Early intervention can reduce unplanned interruptions and support production scheduling.
Critical utilities
Boilers, chillers, compressed-air systems, water-treatment equipment, and other utilities may affect multiple manufacturing areas. Predictive monitoring can identify declining performance before it leads to a broader operational interruption.
For critical utility systems, maintenance priorities should reflect their impact on product quality, validated processes, and facility resilience.
What Role Does AI Play in Predictive Maintenance?
AI can analyze complex relationships across large volumes of equipment data that may be difficult to assess through fixed thresholds alone. Machine learning models can identify unusual operating patterns, distinguish recurring behavior from emerging anomalies, and estimate failure risk when suitable historical data are available.
Different methods serve different purposes. Anomaly-detection models can flag behavior that deviates from normal conditions, while supervised models can learn from labeled examples of known faults. Time-series forecasting can help identify gradual deterioration in measurable parameters.
AI may also help maintenance teams prioritize alerts by combining equipment condition with asset criticality, failure history, and production schedules.
However, sophisticated models are not automatically more reliable. Pharmaceutical manufacturers need to evaluate false alarms, missed failures, data quality, model performance, and the consequences of incorrect recommendations. Human review remains important, especially when maintenance decisions affect critical equipment or product quality.
How Does Predictive Maintenance Support GMP Compliance?
Good Manufacturing Practice (GMP) requires pharmaceutical manufacturers to maintain appropriate equipment, control manufacturing processes, and document relevant activities. Predictive maintenance can support these objectives by providing earlier warnings of deterioration and helping teams plan interventions before equipment performance becomes unacceptable.
Monitoring data may also strengthen maintenance records, identify recurring failures, and support investigations into equipment-related deviations. When connected appropriately to computerized maintenance management systems (CMMS), alerts can help initiate work orders and create a traceable maintenance history.
Predictive maintenance does not, by itself, demonstrate GMP compliance. Manufacturers must establish procedures for evaluating alerts, approving maintenance work, assessing equipment impact, and documenting decisions.
Where equipment is part of a qualified or validated system, changes, repairs, and post-maintenance checks must follow applicable quality procedures. Computerized systems and data used in regulated activities may also require appropriate validation, access controls, audit trails, and data-integrity safeguards based on intended use and risk.
Can Predictive Maintenance Reduce Manufacturing Costs?
Unplanned equipment failures can generate costs beyond replacement parts and repair labor. Production interruptions may delay batches, reduce line utilization, require additional investigations, and disrupt supply commitments.
Predictive maintenance can reduce some of these costs by allowing teams to plan interventions around production schedules, organize spare parts in advance, and focus resources on assets showing signs of deterioration. It may also reduce unnecessary maintenance when evidence supports extending service intervals.
Nevertheless, savings are not guaranteed. Sensors, connectivity, software, integration, model development, and employee training require investment. Poorly calibrated systems can generate excessive alerts, creating additional work rather than reducing it.
Manufacturers should evaluate performance using measures such as unplanned downtime, mean time between failures, mean time to repair, maintenance costs per asset, repeat failures, and production losses. Baselines and pilot results help establish whether benefits justify the investment.
What Challenges Must Pharmaceutical Manufacturers Address?
Data quality is a foundational challenge. Equipment may come from different manufacturers, use inconsistent naming conventions, or operate through legacy control systems that were not designed for advanced analytics. Incomplete maintenance histories can also limit the ability to train and evaluate predictive models.
Integration creates another obstacle. Connecting monitoring platforms with manufacturing execution systems, CMMS platforms, and plant control infrastructure requires careful architecture and testing. Cybersecurity protections are essential because connected industrial equipment can introduce operational risks.
Organizations must also manage workforce readiness. Maintenance engineers need to understand model outputs, while data specialists need knowledge of equipment behavior and manufacturing constraints. Clear responsibility is required for reviewing alerts, authorizing work, and responding when predictions conflict with established procedures.
Finally, manufacturers must distinguish between operational recommendations and decisions that affect validated processes or product quality. Risk-based governance helps determine the appropriate level of review, documentation, and verification.
How Should Pharmaceutical Companies Implement Predictive Maintenance?
A focused, risk-based pilot is often more practical than deploying predictive maintenance across an entire facility immediately.
Manufacturers should begin by identifying assets with frequent failures, high downtime costs, long replacement lead times, or significant implications for product quality. They should assess existing sensor availability, maintenance records, failure modes, and the feasibility of collecting reliable data.
The pilot should establish measurable objectives and compare performance against a baseline. Teams can then select suitable monitoring technologies, define alert thresholds, determine escalation procedures, and integrate approved actions into existing maintenance workflows.
Cross-functional participation is important. Engineering, maintenance, manufacturing, quality assurance, IT, and automation teams should agree on how alerts are assessed and how interventions are documented. Quality involvement is particularly important when equipment supports critical process parameters or validated operations.
Before expanding deployment, companies should evaluate prediction accuracy, false-alert rates, downtime reduction, maintenance costs, and the operational workload created by the system. Successful pilots can inform wider implementation and asset-specific maintenance strategies.
What Is the Future of Predictive Maintenance in Pharma?
Predictive maintenance is likely to become more closely integrated with digital manufacturing platforms, digital twins, and AI-enabled production planning. Digital twins may help teams explore equipment behavior under different operating conditions, while connected systems can link maintenance requirements with production schedules and spare-parts availability.
More advanced platforms may support increasingly automated workflows, from anomaly detection to work-order recommendations. However, autonomous execution requires careful boundaries, human oversight, cybersecurity controls, and appropriate quality review.
The long-term opportunity is not simply predicting failures more accurately. It is coordinating maintenance, manufacturing, quality, and supply planning around a shared understanding of equipment condition and operational risk.
Conclusion
Predictive maintenance offers pharmaceutical manufacturers a practical way to improve equipment reliability, reduce avoidable downtime, and strengthen operational planning. AI and connected sensors can reveal early signs of deterioration, but their value depends on reliable data, sound engineering judgment, and integration with established quality systems.
For pharmaceutical leaders, the priority is to target critical assets, establish measurable outcomes, and scale only after demonstrating operational value. Implemented through a risk-based approach, predictive maintenance can become an important capability in more reliable, efficient, and digitally mature pharmaceutical manufacturing.
Predictive Maintenance in Pharmaceutical Manufacturing
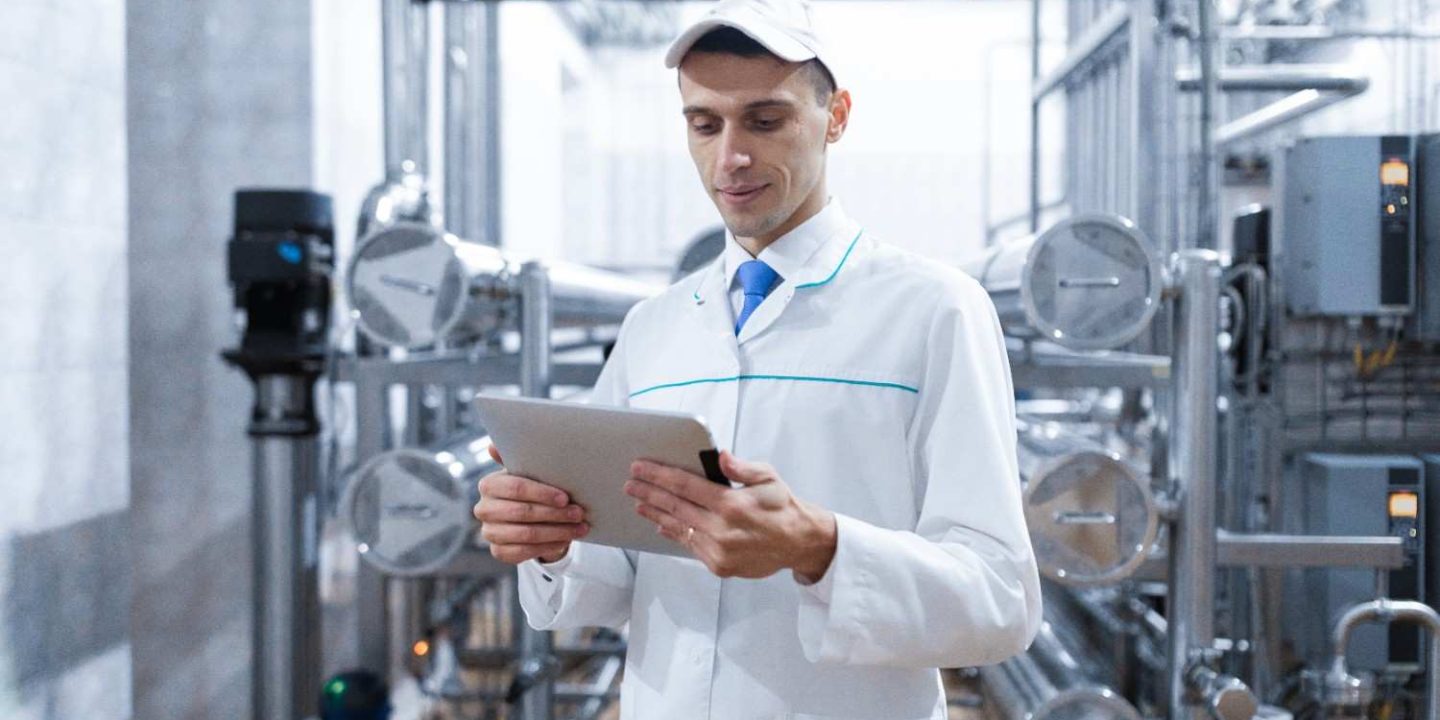
Predictive maintenance is becoming an important strategy for improving reliability, efficiency, and product quality across the Pharmaceutical manufacturing industry. Production facilities depend on complex equipment, including reactors, pumps, compressors, filling machines, packaging lines, and temperature-control systems. Unexpected equipment failures can interrupt production, increase operating costs, and create challenges for meeting strict quality and regulatory requirements.
Traditional maintenance strategies often rely on fixed schedules or repairs after equipment breaks down. Predictive maintenance offers a more proactive alternative by using equipment data, sensors, and analytical tools to identify potential problems before they cause significant disruption.
For Pharmaceutical manufacturers, this approach can help reduce unplanned downtime, improve equipment performance, and support consistent production. When implemented alongside established quality systems and maintenance procedures, predictive maintenance can contribute to more resilient manufacturing operations.